
EDM Sectioning
Precision cutting for advanced inspection and metrologyPrecision sectioning · internal inspection
EDM sectioning for internal inspection
Expose the surfaces you cannot reach from the outside.
Delta XD combines precision wire EDM sectioning with optical 3D scanning and dimensional inspection, so engineers can examine internal geometry against component, CAD and drawing requirements.
Discuss an EDM projectA joined-up inspection workflow
Make internal features measurable
Wire EDM gives controlled access to internal surfaces in electrically conductive components. The cut is planned around the inspection question, then exposed geometry can be captured and assessed using optical measurement.
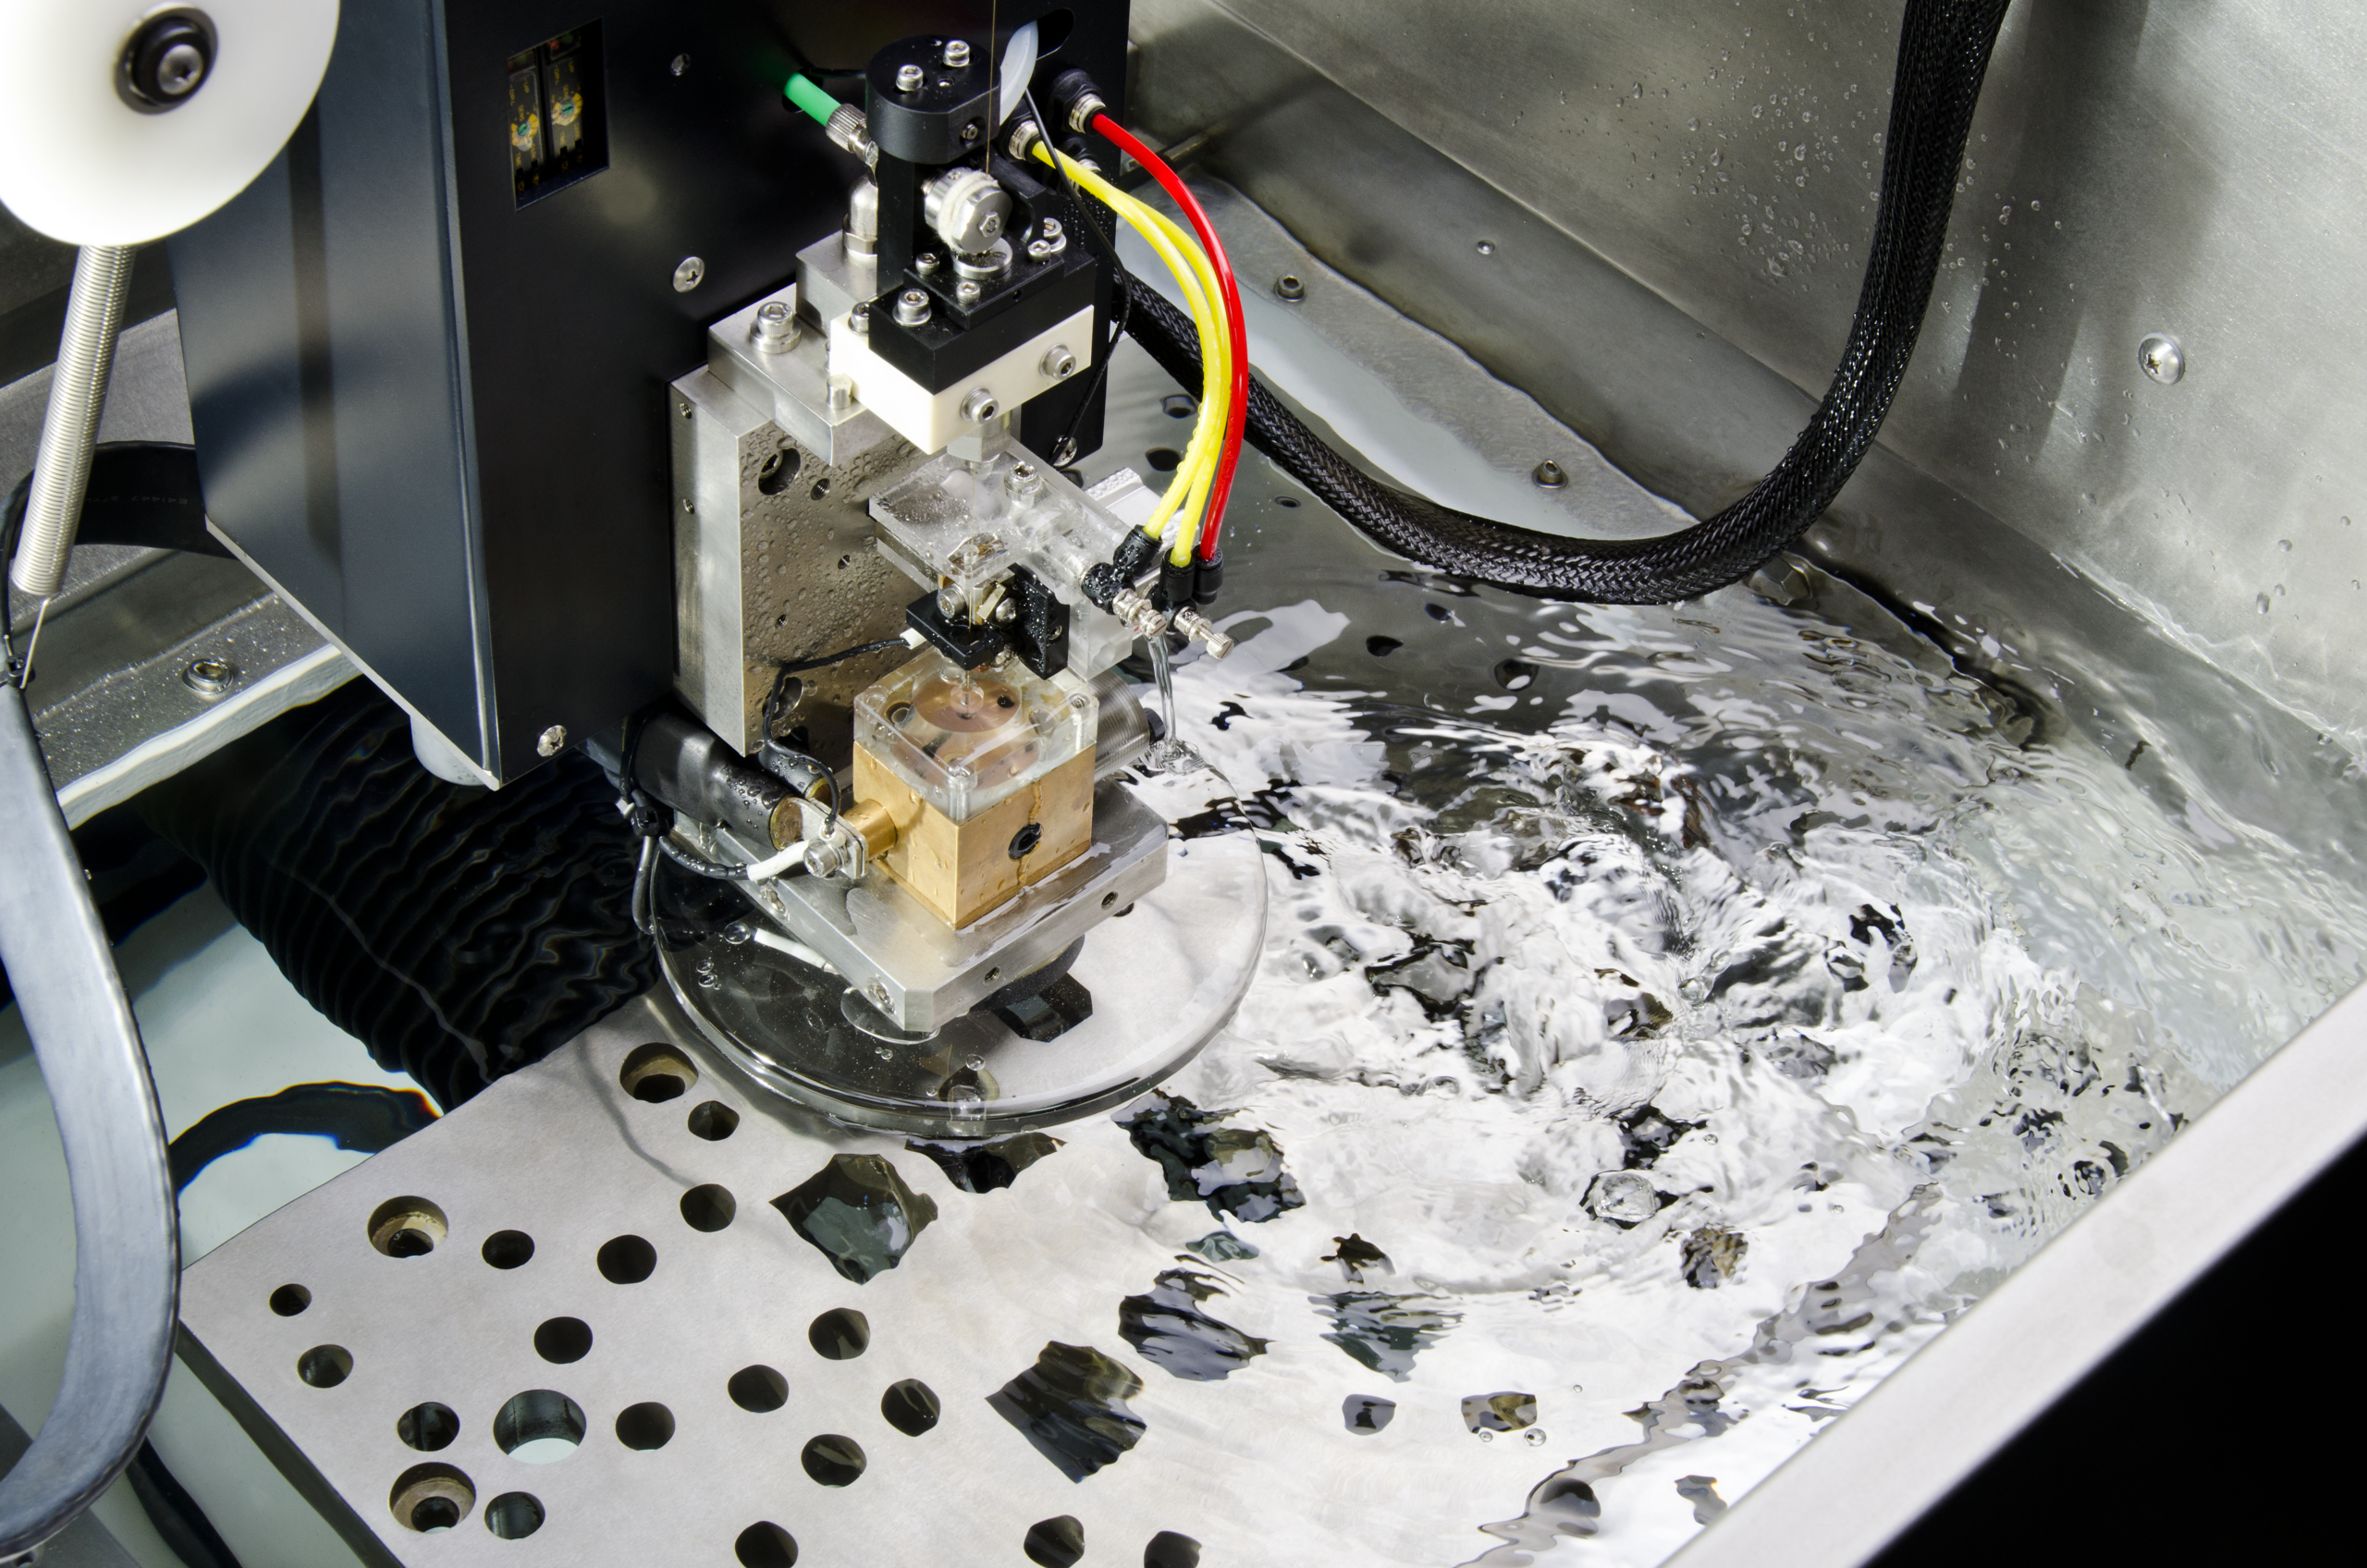
Expose the required feature
Section the component to access internal cavities, cooling passages, wall geometry, core position, profiles or feature locations.
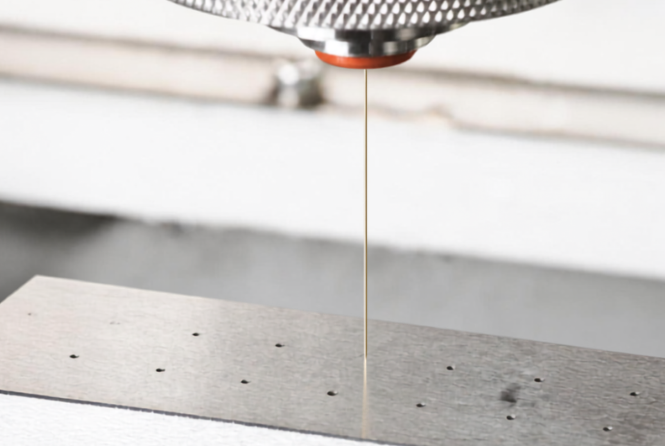
Capture the opened surfaces
Scan newly exposed areas and align them with original measurement data for dimensional inspection and comparison with CAD or drawings.
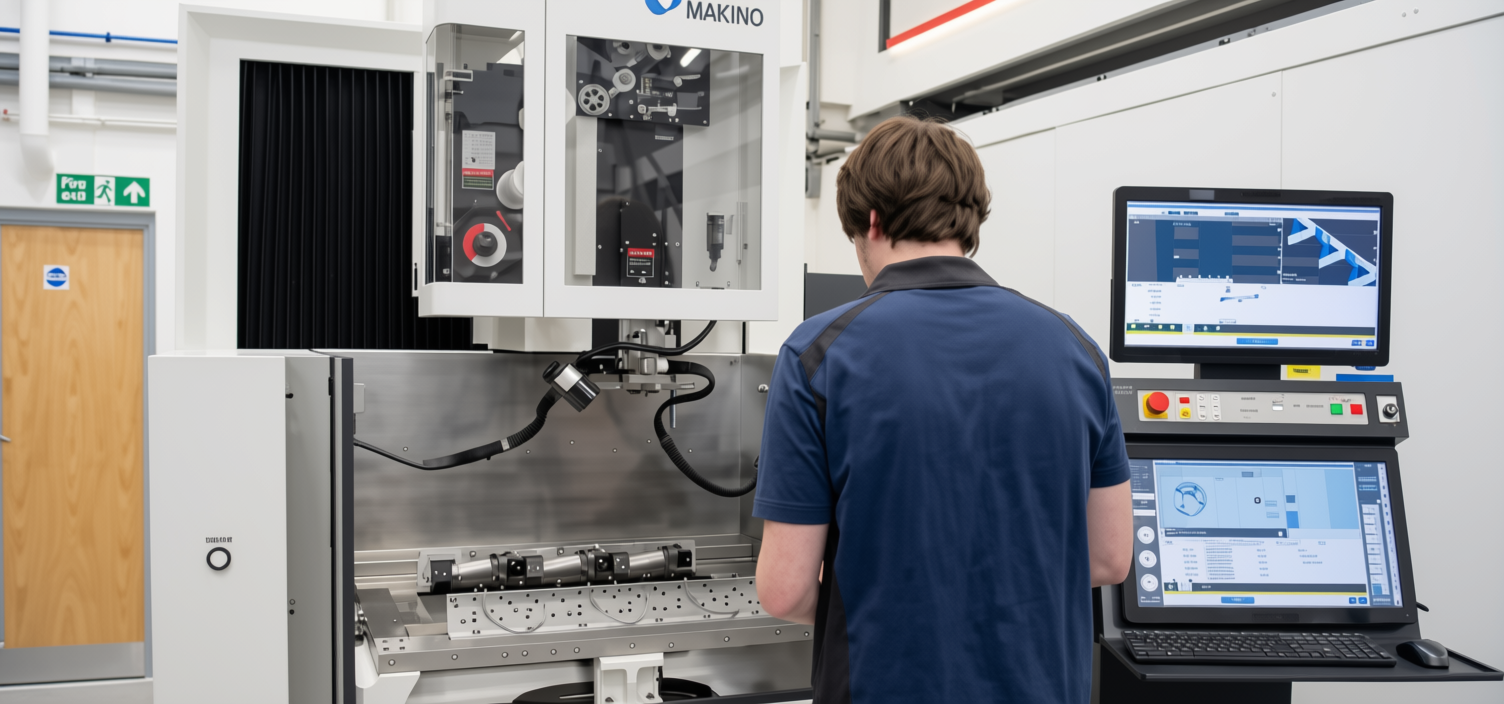
Build evidence for decisions
Use the resulting measurement data to assess internal characteristics, support dimensional validation or contribute to FAI where requirements allow.
Plan · cut · inspect
Measure twice. Cut once.
The complete component is measured first, so the section position can be checked before material is removed.
Define the inspection requirement
Scan and validate section position
EDM section the component
Scan newly exposed surfaces
Align, inspect, compare and report
Keeping sectioning and dimensional inspection together gives Delta XD control over the relationship between the cut, the component and the measurement data, and reduces third-party handling.
Wire EDM capability
Plan around the part and the inspection
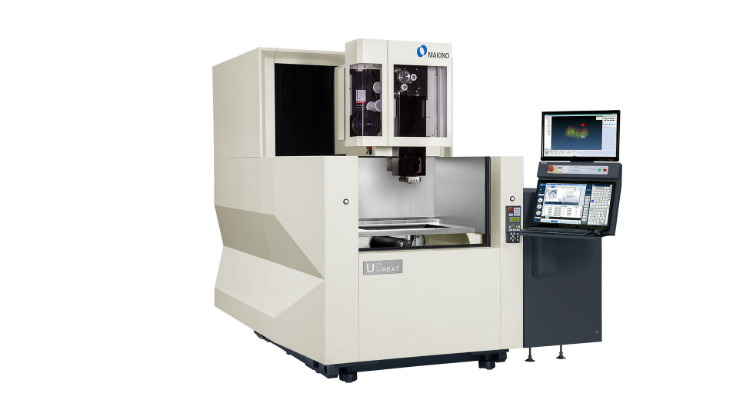
Our Makino U6 H.E.A.T. Wire EDM is used for intricate components and larger castings. Cutting strategy is selected around geometry, access and material loss.
Wire EDM works with electrically conductive metals regardless of hardness, including steels, aluminium, titanium and nickel-based alloys. Wire down to 0.10 mm diameter can be used where minimising material loss is important. For complex geometry, 3D scanning can inform adaptive machining and 3D cut paths.
When original CAD is missing
More of the part in the digital model
For legacy, obsolete or one-off components, EDM sectioning can add internal geometry to a reverse engineering project. Recording the external form before cutting and scanning hidden surfaces afterwards gives engineers more measured information for CAD reconstruction.
Sectioning is destructive. The cut plan should be agreed against the part, inspection need and drawing or specification requirements before work begins.
Common questions
EDM sectioning, explained
Can EDM inspect turbine blade cooling passages?
Yes. EDM sectioning can expose cooling passages, wall geometry, cavities and other internal features within electrically conductive turbine components for measurement using optical 3D scanning.
When might EDM sectioning be considered instead of industrial CT?
It may be considered when component size, material, density or required resolution makes industrial CT impractical or expensive. EDM is destructive, but gives direct access to internal surfaces for high-resolution measurement.
Can sectioning support First Article Inspection?
Sectioning and dimensional measurement can provide data for otherwise inaccessible features as part of an FAI, subject to the component drawing, specification and applicable requirements.
How much material is lost?
Material loss depends on wire diameter, spark gap and cutting strategy. The resulting cut width is known as the kerf. Wire down to 0.10 mm diameter can be used where minimising material loss is important.
What materials can wire EDM cut?
Wire EDM can cut electrically conductive metals, including steels, aluminium, titanium and nickel-based alloys.
Can Delta XD provide standalone EDM cutting?
Yes. EDM is primarily integrated with 3D scanning, inspection and metrology, and standalone precision EDM cutting and component sectioning can also be provided where required.
Our in-house Wire EDM capability allows us to precisely section complex components, providing access to internal features and surfaces that would otherwise be difficult to measure.
Using the Makino U6 H.E.A.T. Wire EDM, we can combine precision sectioning with 3D scanning and dimensional inspection to create a complete metrology workflow, from the initial measurement of a component through to detailed inspection of its internal geometry.
Why EDM Precision Sectioning?
-
Access internal geometry for detailed measurement and inspection
-
Extremely precise cutting with minimal material loss
-
Section large, complex or difficult-to-inspect components
-
Reduce the number of cuts and subsequent digital reconstruction required
-
Combine EDM with 3D scanning and dimensional inspection
-
Suitable for complex and difficult-to-machine materials
Precision cuts. Better inspection data.
Our Makino U6 H.E.A.T. Wire EDM allows us to accurately control where and how a component is sectioned.
The machine can cut to four microns and use wire down to 0.10 mm diameter where minimising material loss is important. Alternative wire sizes and cutting strategies allow us to balance precision, material loss and cutting time around the individual component and inspection requirement.
For complex geometry, we can also combine 3D scanning with adaptive machining to create 3D cut paths, giving us greater flexibility over how internal features are accessed.
Measure Twice, Cut Once
The complete component is scanned to validate the required section position before cutting. Once sectioned, newly exposed surfaces can be captured using optical 3D scanning and aligned with the original measurement data for dimensional inspection and CAD comparison.
Determine Section Position → 3D Scan & Validate → Precision Cut → Scan Internals → Digitally Assemble → Inspect, Compare & Report
Keeping the complete process with Delta XD also reduces third-party handling and lead times, while giving us control over the relationship between the cut, the component and the resulting measurement data.
Built for components of all sizes
With a 650 × 450 × 420 mm working area and maximum workpiece size of 1,000 × 800 × 400 mm, our EDM capability accommodates everything from intricate components to larger castings.
The machine can produce tapers of ±15° as standard, with angles up to 45° possible following prior discussion, and can achieve a surface finish of <2.5 Ra.
Wire EDM works with electrically conductive metals regardless of hardness, making it suitable for steels, aluminium, titanium and difficult-to-machine nickel-based alloys.
From inspection to Reverse Engineering
EDM also expands the data we can capture when reverse engineering components with little or no original CAD.
By recording the external geometry before sectioning and scanning previously hidden surfaces afterwards, our engineers have more information available to reconstruct the complete component in CAD.
This can be particularly useful for legacy, obsolete or one-off parts where only a single physical example is available.
What Can We Inspect
Precision sectioning can support dimensional inspection of internal cavities, cooling passages, wall thickness, core position and core shift, internal profiles and feature locations.
This makes the process particularly relevant to turbine blades, investment castings and other complex components within the aerospace, automotive and casting industries.
The resulting measurement data can be used for dimensional validation, CAD comparison and First Article Inspection (FAI) where inaccessible internal characteristics need to be assessed.
